A crossbody purse wholesale program lives or dies on structure, not on a single hero style. Retail buyers who reorder consistently plan the category around three layers: a range of sizes and closures that cover distinct daily-carry needs, a short list of construction checkpoints every sample must pass, and a branding workflow locked down before mass production. This guide walks through those three layers, using two reference builds from the Wellmax Luggage catalog as concrete examples.
Planning size and compartment structure for daily-carry programs
Crossbody purses occupy a narrow but crowded space: the bag must hold a phone, cards and a few personal items without becoming bulky against the body. When planning an assortment, the useful question is not "how many SKUs" but "which daily-carry problems does the range cover." A workable structure usually separates the range into a slim, flat silhouette for minimal carry; a mid-size body with one interior divider or a back slip pocket for phones plus sunglasses; and a flap-front style that reads more formal for work-to-dinner use. Three silhouettes per color story, in two or three colorways each, is a manageable depth for a first order.
Compartment planning should be specified on the technical sketch, not left to the factory's judgment. Pocket count and position, lining color, divider placement and closure type all change cost and production complexity, so writing them into the spec sheet prevents ambiguity at quotation. Wellmax's catalog illustrates the two ends of that spectrum. The Crossbody Flap Handbag is a PU leather build with a flap secured by a magnetic snap, offered in black, camel and tan. The Nylon Shoulder Crossbody Bag is a lightweight nylon build with a zipper closure and an adjustable crossbody strap, offered in beige, black and navy. A zip closure suits buyers who prioritize security; a magnetic flap suits buyers prioritizing one-handed access and a dressier silhouette. Both catalog builds carry an MOQ from 500 pcs per style and a standard lead time of 30-35 days after sample approval and order confirmation, which makes them realistic anchors for a mixed program rather than aspirational placeholders.
The two styles also differ in packaging: the flap handbag ships in an individual dust bag plus export carton, the nylon style in an individual poly bag plus export carton. Dust bags add perceived value but also bulk per unit, which matters most for gift-oriented retail.
Construction checkpoints to specify before sampling
Small bags fail at predictable points, and those points can be written into the specification as checkpoints a sample must pass before approval: strap attachment, stitch density, zipper function and hardware finish.
Strap attachment is the load-bearing element of a crossbody. Because the entire bag weight hangs from two anchor points, buyers should specify how the strap joins the body — stitched through reinforced panels, box-and-cross stitching, or additional rivets where the design allows — and how many stitch lines anchor each junction. On adjustable straps, as used on the nylon catalog build, the slider and the buckle-end fold should also be inspected, since an under-stitched fold will slip under load. Stitch density is the second checkpoint: a general rule for bags is a consistent stitch count per centimeter agreed in the spec, with straight, even tension lines along the strap edges and stress points back-tacked rather than left loose.
Zipper function is checked on every approved sample and again at inspection: the pull should run the full travel without catching at either end, and the slider should hold closed under light lateral pressure. Hardware finish covers color consistency across plating batches, absence of sharp edges, and plating that survives a rub test without flaking. For the PU flap handbag, the magnetic snap deserves its own check — the closure should engage positively without excessive force, because a weak snap shows up quickly in retail returns.
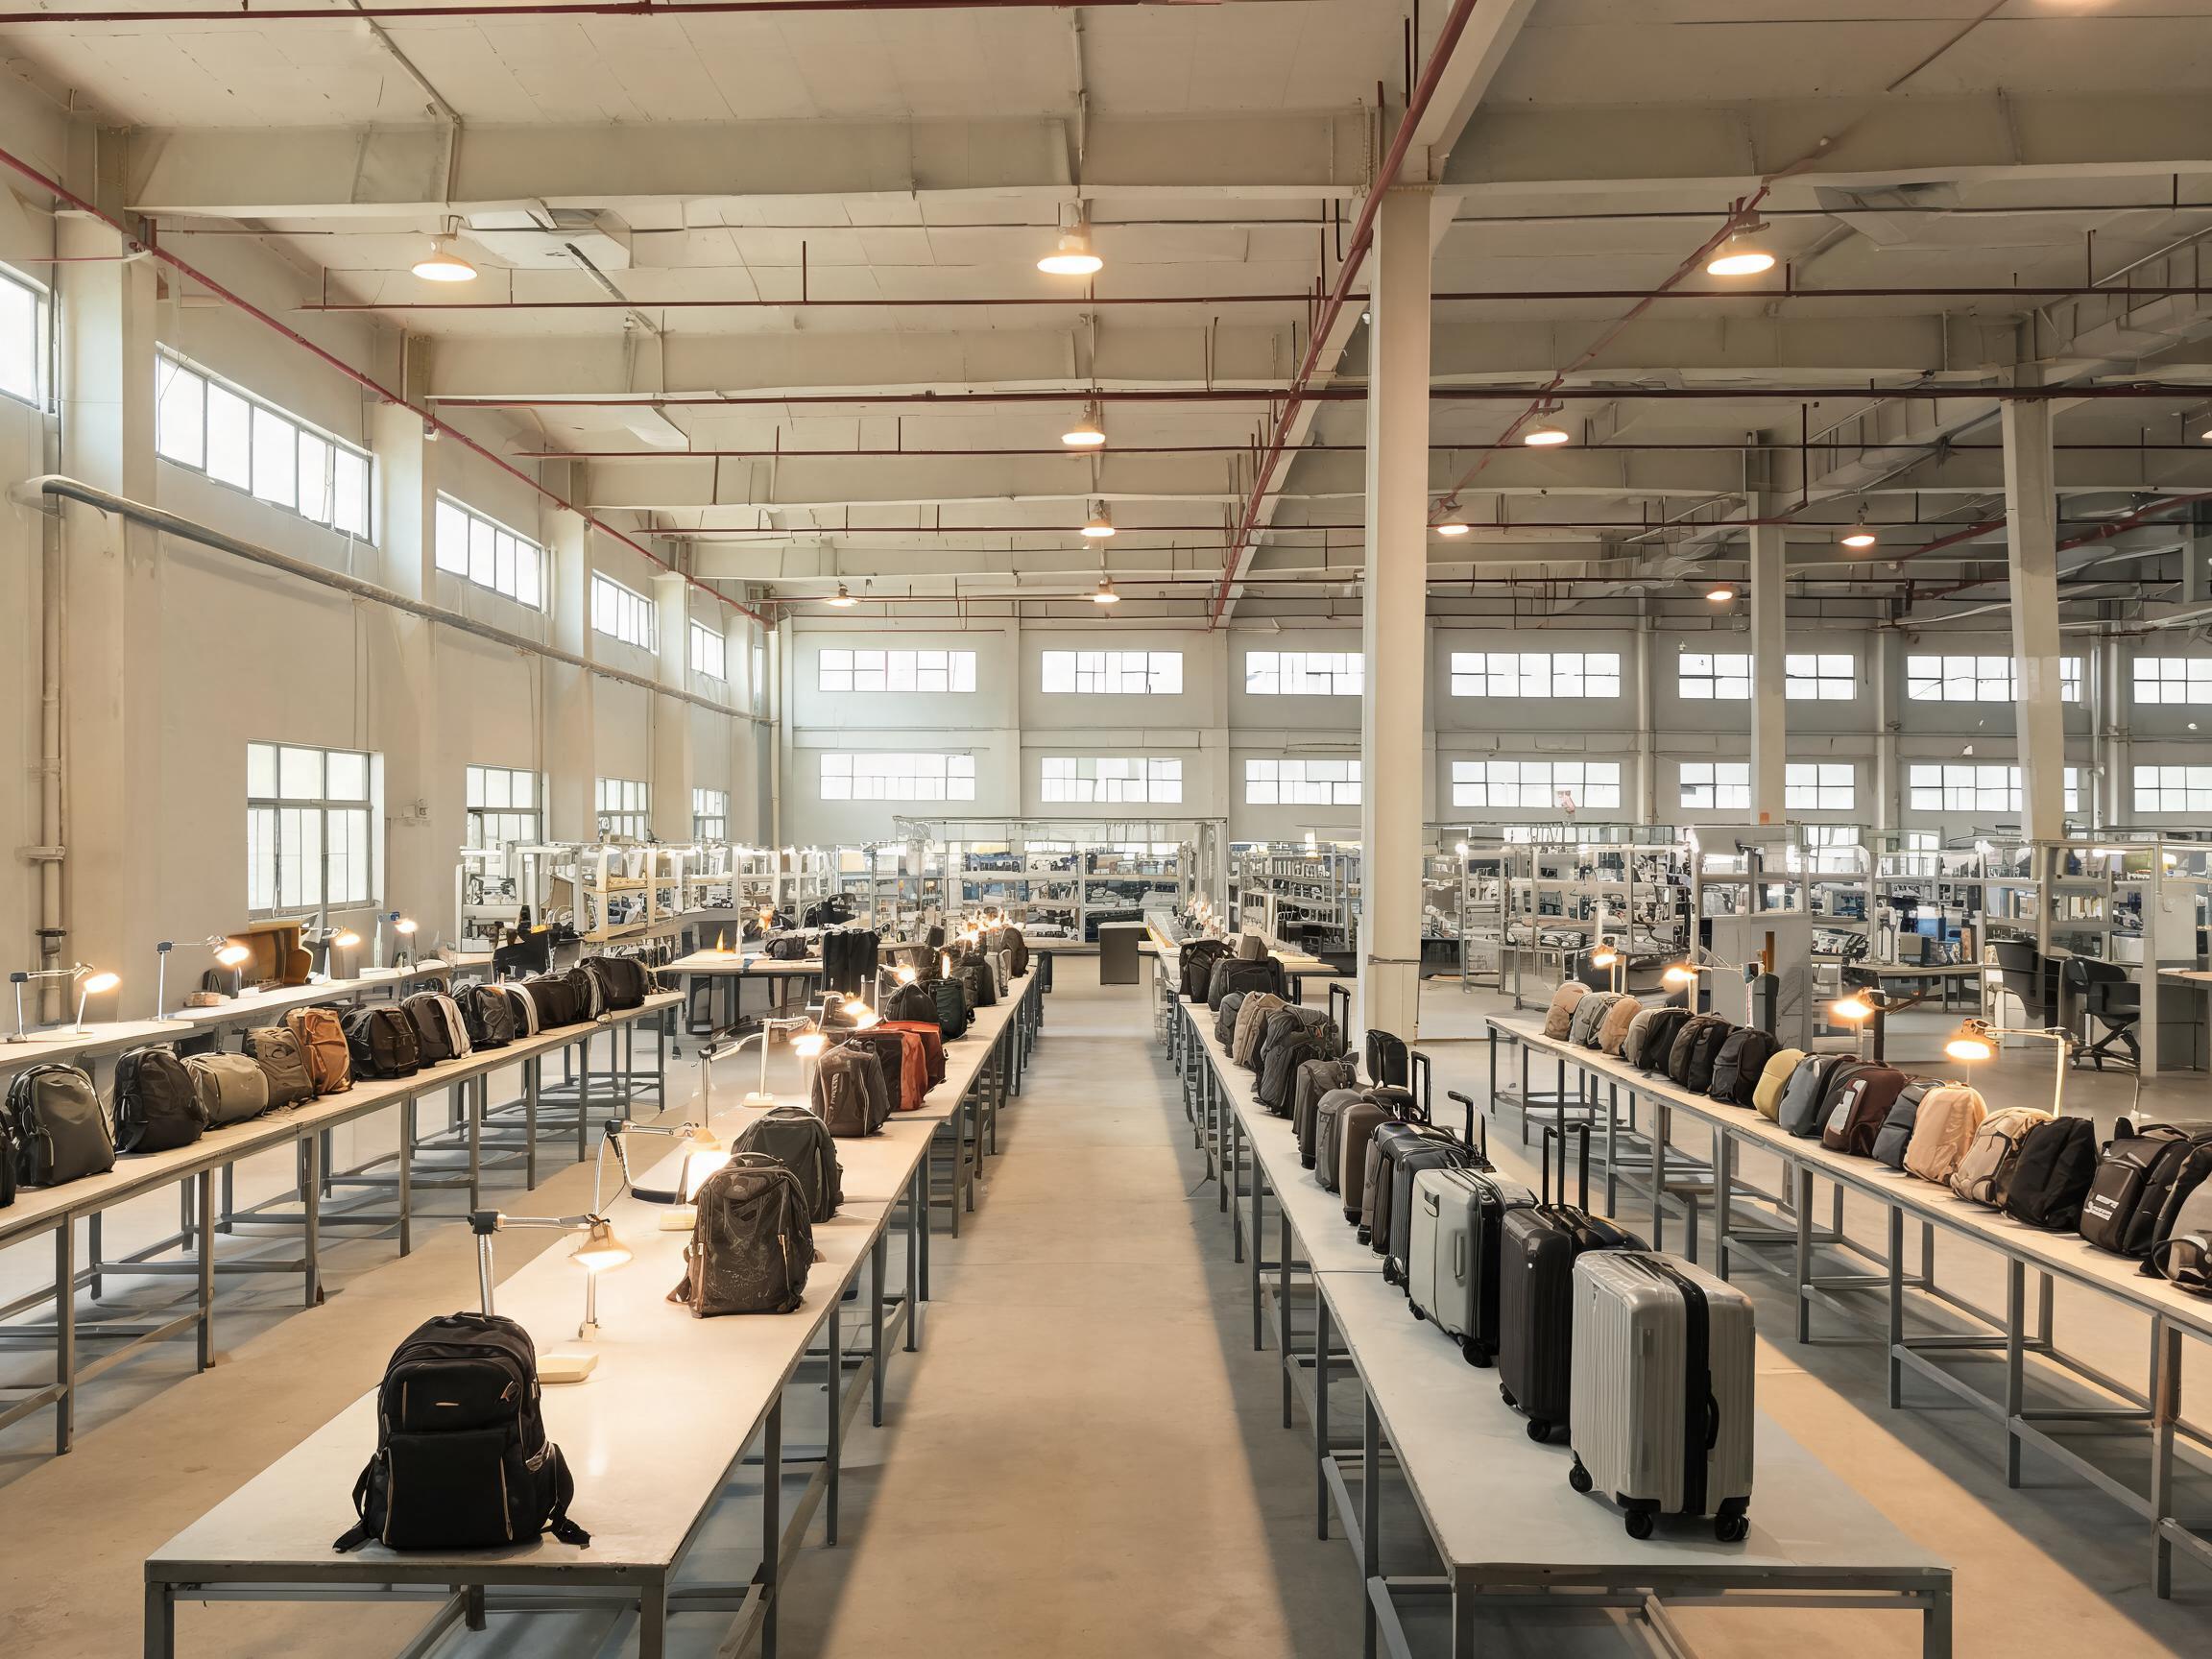
Written into the spec sheet, these checkpoints give the factory an unambiguous quality target before cutting begins and give your inspector a defined pass/fail list for the finished order. Third-party inspection and buyer-specified Incoterms can be arranged on request under Wellmax's baseline ordering terms, to be confirmed per style and program.
Branding on a small surface: options and trade-offs
Crossbody purses are small, which limits how much logo space a buyer has to work with. The realistic branding options, and where each performs best, are:
| Method | Best suited to | Practical note |
|---|---|---|
| Woven label | Interior or seam branding; detailed logos | Sews in during assembly; durable and low-key |
| Rubber patch | Sport and nylon builds; raised 3D logo | Suits casual programs and bold brand marks |
| Screen printing | Flat nylon panels; simple marks | Lowest tooling cost; limited detail on textured surfaces |
| Heat transfer | Multi-color logos on nylon and PU | Check adhesion on coated fabrics during sampling |
| Embroidery | Small marks on heavier fabrics and PU panels | Premium look; can pucker lightweight nylon |
The nylon catalog build documents this directly: customization covers nylon type and denier, strap width and hardware, pocket count and dividers, and branding by woven label, rubber patch, screen printing or branded packaging, with branding quoted on request. On the PU flap handbag, customization of color, lining and hardware is confirmed before sampling — meaning hardware finish can be matched to the brand's metal standard if it is specified early. Because all five methods change tooling and unit cost differently, the decision should be made before the sample is made, not after it.
The OEM sampling workflow, from spec sheet to approved sample
A disciplined sampling sequence keeps a 30-35 day lead time achievable. In practice the workflow runs as follows:
1. Spec sheet. The buyer submits dimensions, material and denier (for nylon builds), lining color, pocket and divider count, closure type, strap width, hardware finish and branding method with artwork. Wellmax's catalog explicitly lists which customizations are confirmed before sampling, so anything missing from the spec will surface as a question at this stage.
2. Quotation. With the spec fixed, the export sales team prices the style. Branding is quoted on request, so artwork format and placement should accompany the RFQ. Material choice drives both price and MOQ tiers; see the guide on material grades and MOQ tiers.
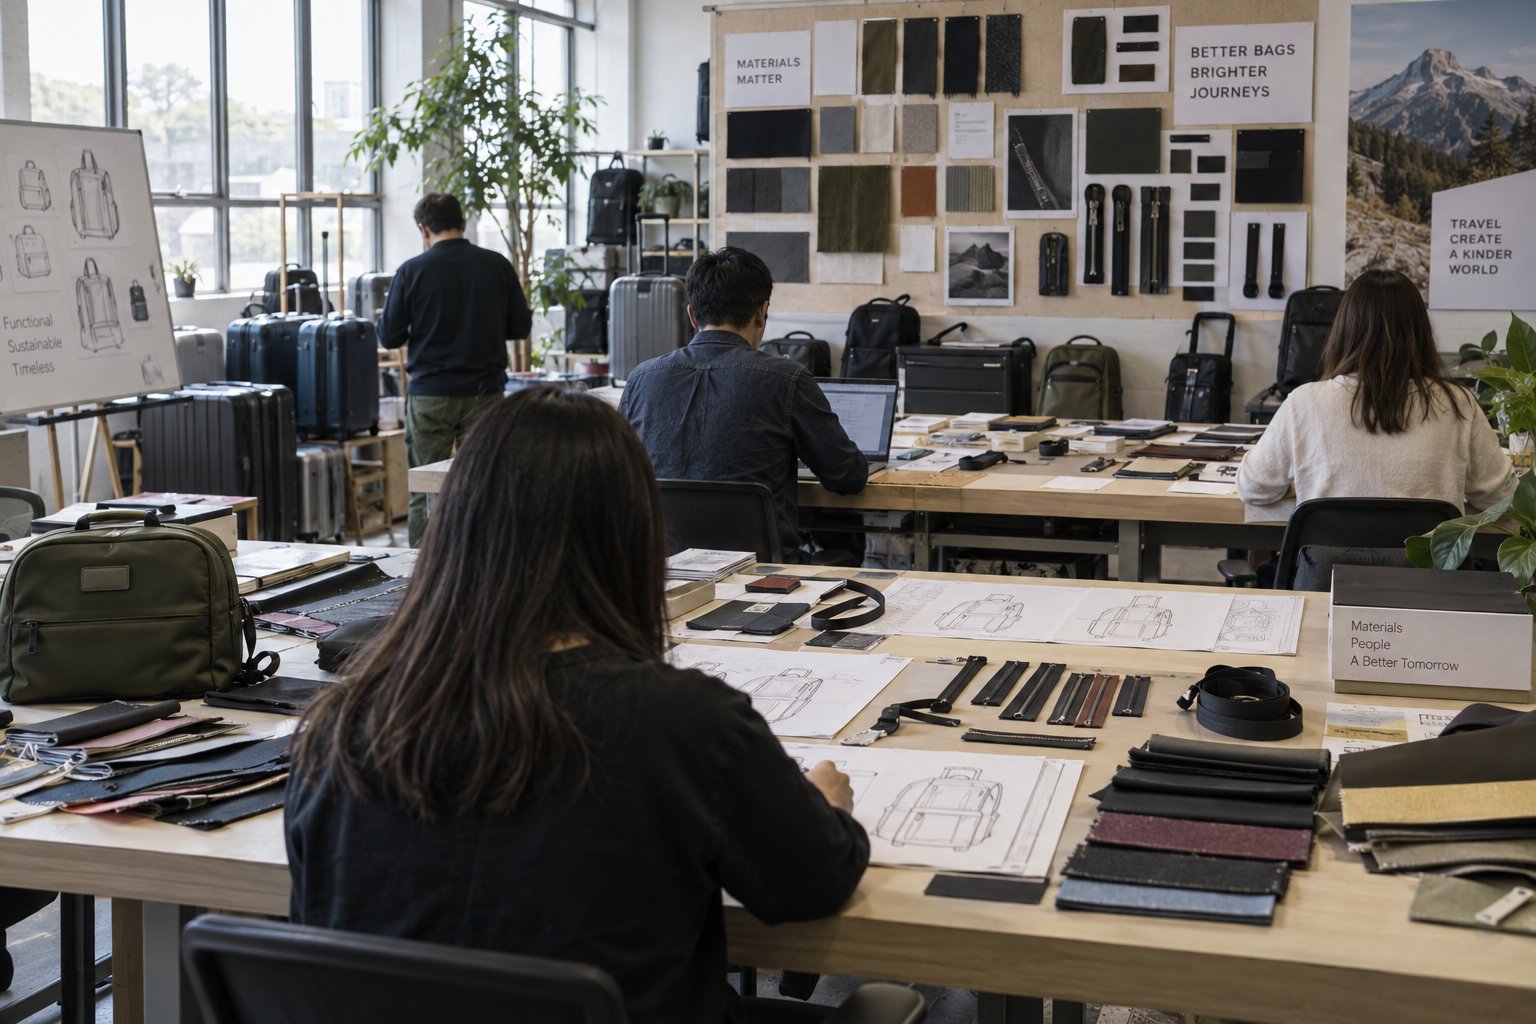
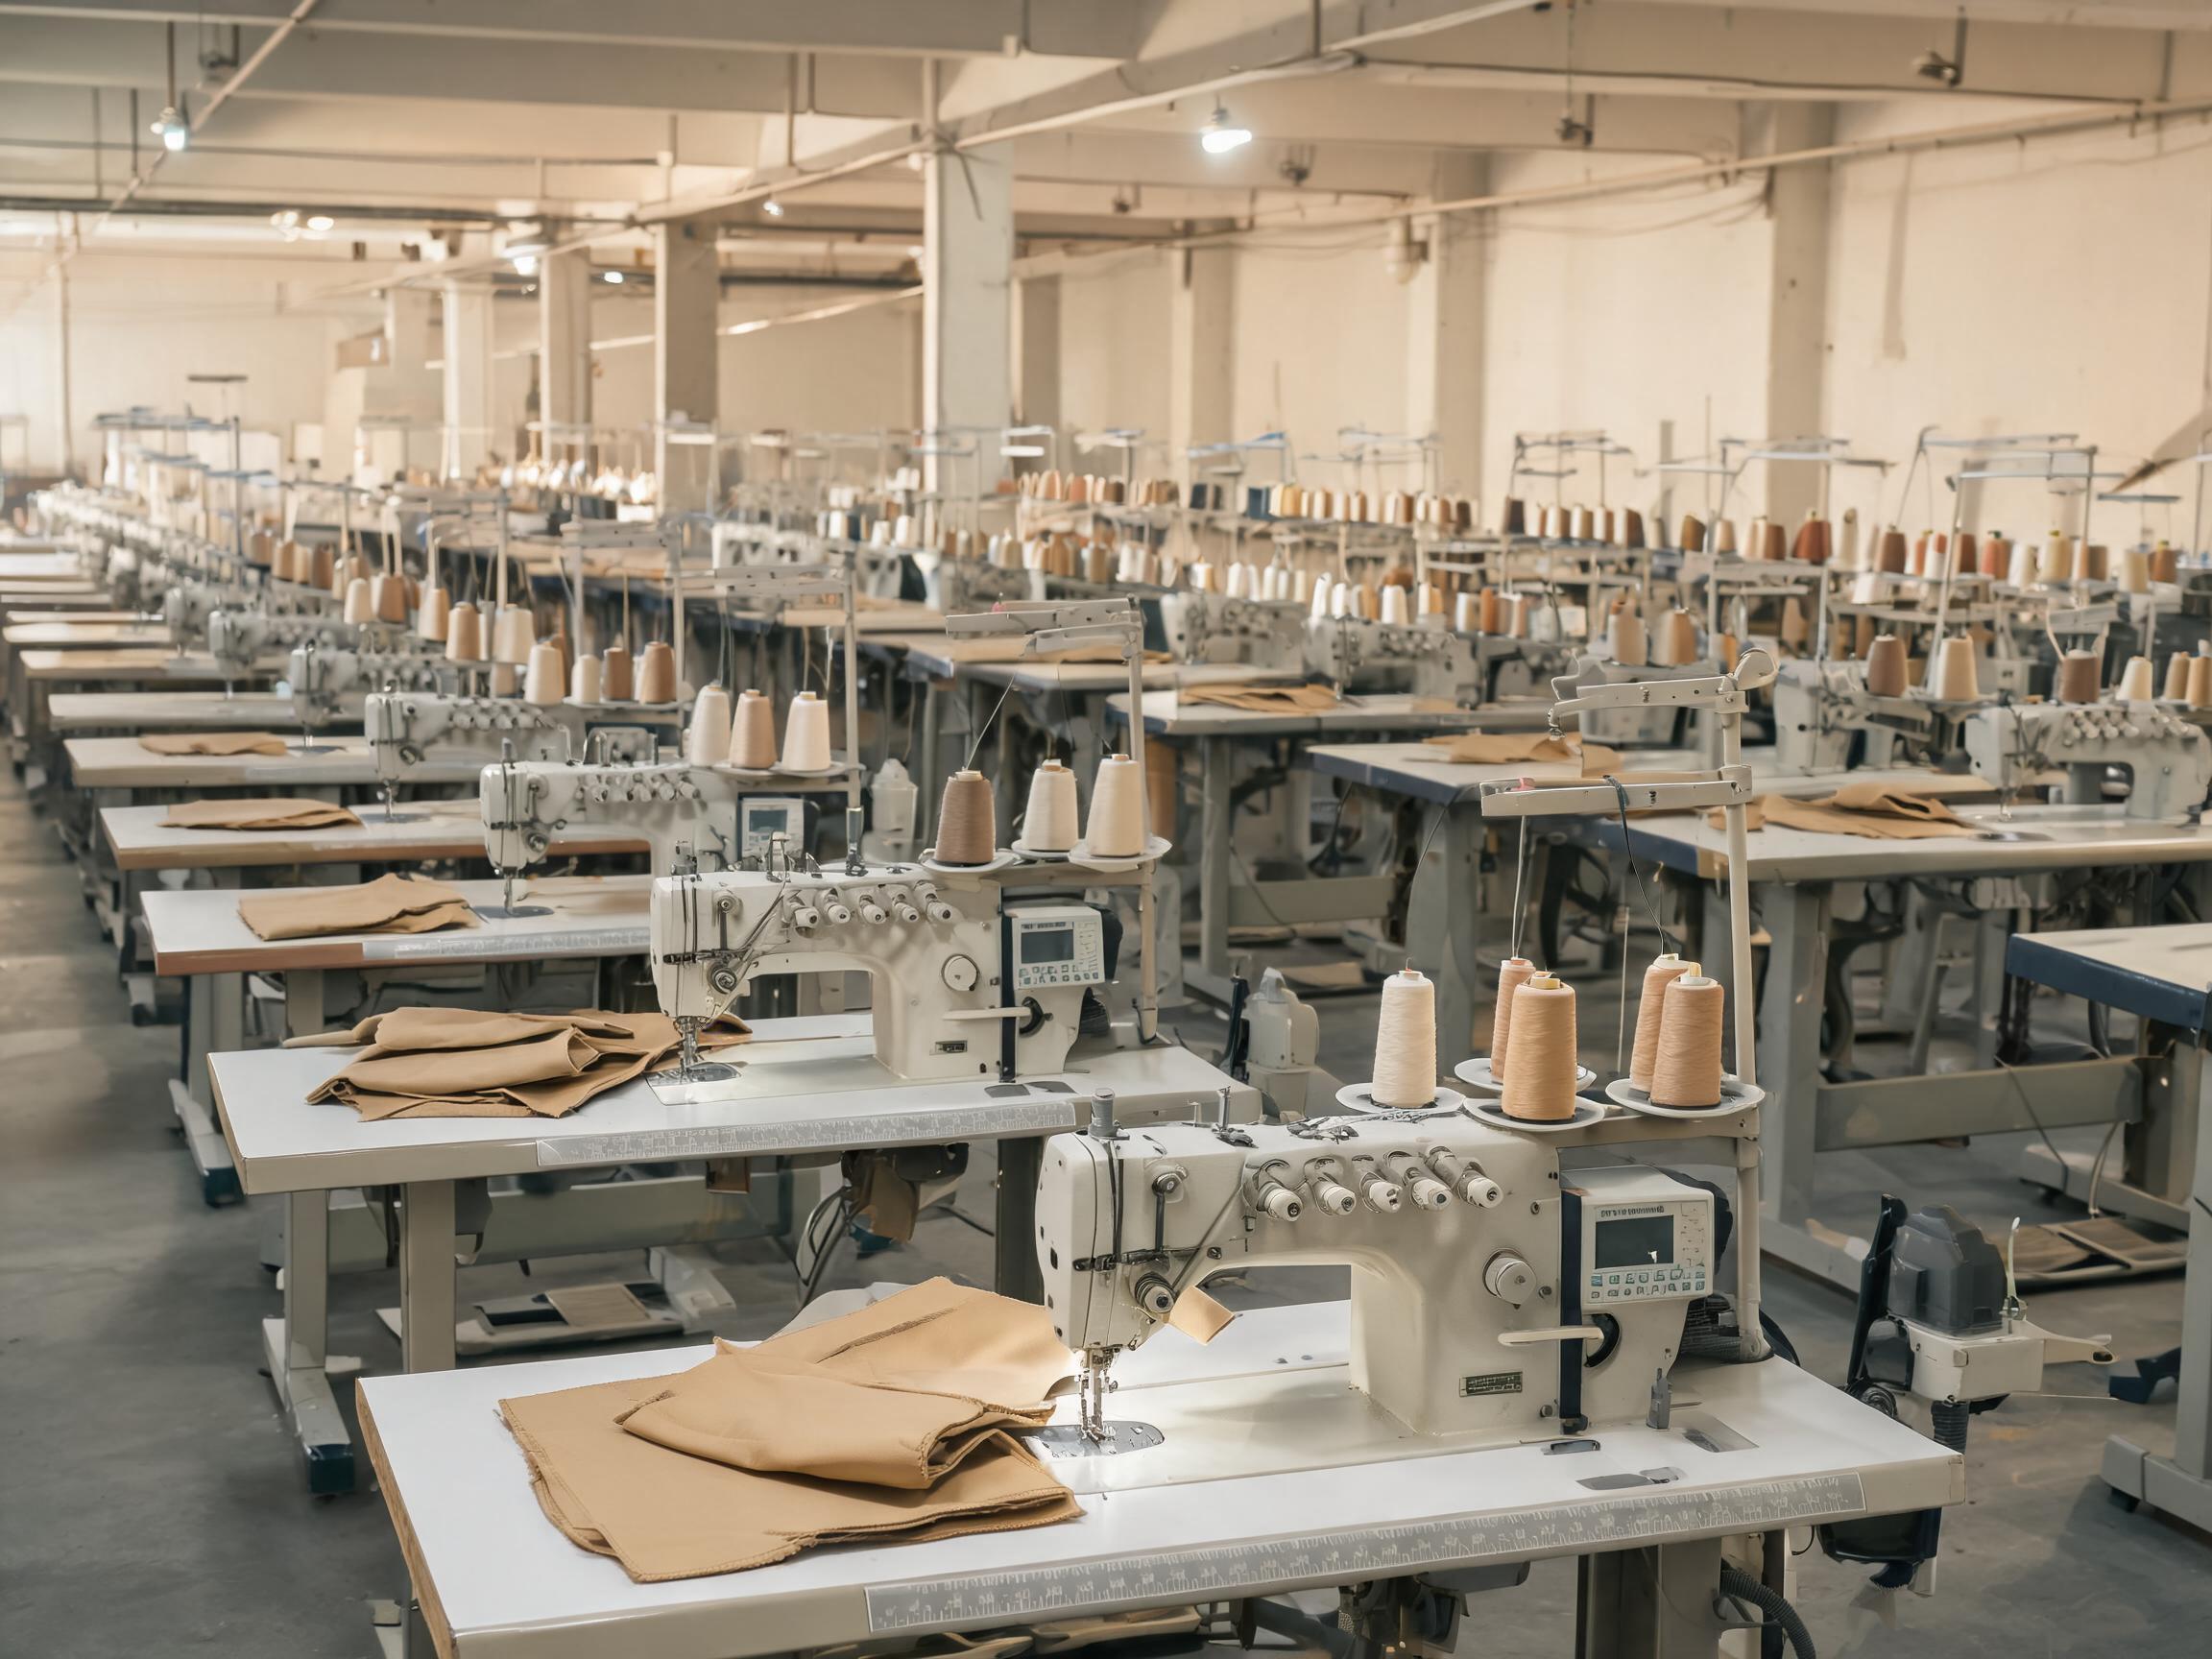
3. Pre-production sample. The factory cuts, sews and assembles a sample to the spec, in the in-house studio and workshop. The buyer checks the strap attachment, stitch density, zipper travel and snap engagement, hardware finish and branding execution against the agreed checkpoints, then approves or returns comments. Each revision round adds time, which is why an ambiguous spec is the most common cause of a stretched program calendar.
4. Approved sample and mass production. Once the sample is approved and the order confirmed, production proceeds to the standard 30-35 day window, with quality inspection and export handling under the same roof. Third-party inspection can be booked if the buyer's program requires it.
Category mix and replenishment cadence for retail programs
An assortment built only for launch will age poorly. A healthier retail program balances depth in proven silhouettes against a small rotation of seasonal colorways. With an MOQ from 500 pcs per style, a buyer can split an opening order across two structural styles and several colorways without over-committing capital to one look. Nylon builds often suit spring and summer rotations and PU flap builds autumn and gifting seasons, though the timing depends on the buyer's channel and market — decide from sell-through data rather than the factory calendar.
Replenishment planning should also account for the full order cycle. Because sampling, tooling, mass production and inspection run in-house at one facility, reorder cycles can be quoted once monthly sell-through is known. A useful comparison of how suppliers structure MOQ, tiers and replenishment programs is covered in the supplier-vetting guide on MOQ, price tiers and replenishment. The practical takeaway is to forecast sell-through by SKU before the first order ships, so the reorder decision is made against real data rather than a launch-season estimate.
For a deeper style-selection discussion that this article deliberately does not repeat, the site's guide on choosing flap and nylon styles for a private-label program compares the two constructions in detail. The handbags category page lists the current crossbody reference builds alongside other handbag styles.
Quality assurance at the supplier level is worth a closing note. Wellmax Luggage operates under an ISO 9001:2015 certified quality management system covering the design, manufacturing and sales of luggage and travel bags, and the Quanzhou facility is audited under the BSCI framework for social compliance. Both are company- and facility-level credentials; they do not certify any specific product, so per-SKU quality still rests on the sampling and inspection checkpoints described above. Buyers planning a crossbody purse program can send a spec sheet or artwork pack to the export sales team for a quotation and sampling plan.